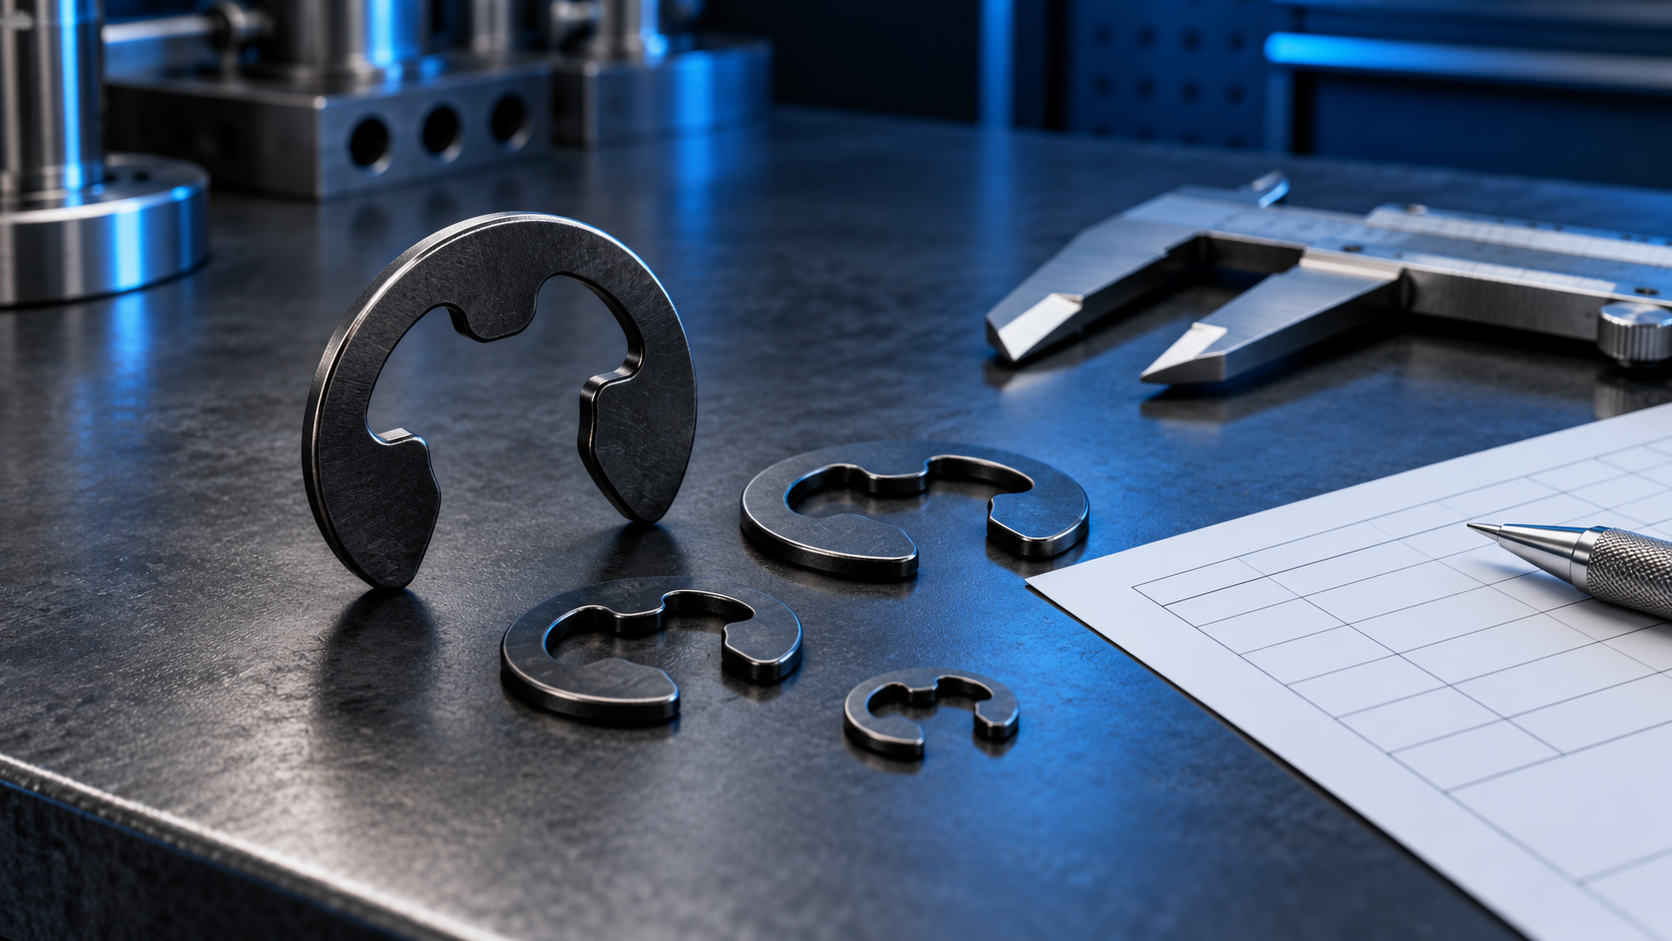
Phosphate coating on steel retaining rings is often described too simply. Phosphate is a conversion layer formed on the steel surface; oil may then be used as a separate protective step. The combination can be useful, but it is not a universal promise of corrosion life. The finish, process and evidence must match the retaining ring and the purchase requirement.
For a buyer searching for phosphate coating steel, the practical question is not only “is it phosphated?” It is “which finish condition was ordered, how is it identified, and what evidence belongs to this lot?”
A phosphate process converts the near-surface metal into a crystalline conversion layer. That layer can support oil retention and provide a defined surface condition, but it should not be described as a thick paint film or as a standalone guarantee against every service environment.
Ask the supplier to identify the specified process and the condition after treatment. If oil is included, record it separately. The order should make clear whether the requirement is phosphate only, phosphate plus oil, black oxide, another finish or no additional treatment.
| Requirement | What it describes | What to confirm |
|---|---|---|
| Phosphate | A conversion coating on the steel surface | Process reference, finish condition and lot evidence |
| Oil | A separate protective film or packaging condition | Whether oiling is included and how it is identified |
| Black oxide | A different conversion-finish route | Applicable standard, post-treatment and corrosion criterion |
These names should not be swapped merely because the parts look dark. A visual check can detect an obvious mismatch, but it cannot replace the finish designation or a process record.
The phosphating process should therefore be treated as part of the controlled finish route. The buyer does not need a chemistry lecture in the RFQ, but does need a clear finish name, post-treatment condition and evidence owner. This is especially important when the same ring family can be supplied for different environments or packaging requirements.
The phrase phosphate coating vs black oxide is useful during selection, but it should not become a promise that one finish always performs better. Compare the specified environment, lubrication, handling and test criterion. If the requirement is only appearance, say so; if it is corrosion evidence, define the test and sample.
DIN 471 identifies the external retaining-ring application and its dimensional and functional boundary. The finish requirement should be read with the applicable edition and the order documentation. Confirm the ring size, material condition, burr condition, surface requirement and any corrosion test requested by the customer.
The DIN 471 external circlip product route can support a sourcing discussion, but it does not turn a product-family page into a lot certificate. A receiving packet should still identify the delivered ring and finish.
Record the ring size, quantity, incoming lot, visible surface condition and packaging condition before the parts enter production. If the finish is phosphate plus oil, note whether the oil is present as supplied and whether the customer has a cleaning or lubrication step that changes the surface before assembly.
When the visual appearance is inconsistent, hold the lot for document review instead of deciding from color alone. Compare the purchase order, finish designation, supplier process record and any corrosion report. This creates a simple chain from requirement to inspection and avoids treating a dark surface as proof of one particular process.
If a salt-spray or other corrosion report is requested, the report should identify the specimen, finish, preparation, exposure method, duration and evaluation criterion. Do not turn a test-hour figure into a service-life promise. The result is meaningful only within the conditions recorded for that specimen.
For an RFQ, a concise request can say: identify the finish condition, state whether oiling is included, provide the applicable process or standard reference, and attach any report that applies to the ordered lot. This is more useful than asking for “rust proof” parts without a defined test or environment.
No. They are different conversion-finish routes. The correct choice depends on the drawing, environment, lubrication and evidence requirement. The supplier should use the finish named in the order rather than substituting a visually similar dark finish.
No. It describes a supplied finish condition, not an unlimited service-life result. Corrosion performance depends on the environment, handling, packaging, exposure and any agreed test criterion.
When the finish affects acceptance, send the ring size, drawing revision and requested evidence through the TG Eugene service route. That keeps the finish decision tied to the actual order.
No external source link is used in the body. The local DIN 471 and finish-reference package is recorded in the article evidence map.